Views: 0 Author: Site Editor Publish Time: 2026-09-15 Origin: Site


Selecting the right packaging format for rope isn't just an aesthetic choice. It directly dictates logistics costs, material integrity, and the required capital investment in packaging machinery. Getting this decision wrong eats into your profit margins daily. For operations and procurement managers, misaligning the winding method with the rope material or end-user application creates massive headaches. It frequently results in material deformation, severe production bottlenecks, and highly inflated shipping overhead. You need a reliable, data-backed strategy to optimize this process.
This guide provides a robust technical and commercial framework to evaluate these methods. You will discover which winding format serves your specific product lines best. We also detail how to specify the exact industrial winding equipment your facility needs. By understanding the mechanical differences between spools, hanks, and coils, you can future-proof your production lines for maximum efficiency.
Application Drives Format: Spools offer structural support for continuous industrial use, hanks suit retail and low-volume dispensing, and coils are optimal for heavy marine or construction ropes.
Tension Control is Non-Negotiable: Insufficient or excessive tension during the winding process degrades material memory, especially in synthetic fibers.
Machinery Scalability: Choosing between a spool winding machine, hank winder, or coil winder requires balancing current throughput needs with future diameter-changeover flexibility.
You cannot select a winding format without first analyzing your material. Different rope constructions behave differently under stress. Material memory, friction coefficients, and elasticity all dictate your final choice. We must look at the specific physical properties of the rope.
Natural fibers present unique characteristics. Materials like sisal or manila possess a rough exterior texture. This creates a high friction coefficient. The rope grips itself easily. You can wind it into unsupported shapes without collapse. Natural fibers also exhibit low elasticity. They do not stretch significantly under normal pulling forces. Therefore, they hold their shape well in bulk configurations.
Synthetic fibers present a completely different challenge. Ropes made from UHMWPE (Ultra-High-Molecular-Weight Polyethylene) or nylon are incredibly slick. They feature a very low friction coefficient. The layers tend to slide against one another. If you coil them loosely, the package often collapses. They require rigid structural support to maintain integrity. Synthetic fibers also possess distinct material memory. They easily remember the shape they are forced into. Over-tensioning them causes permanent deformation.
You must also consider end-user dispensing needs. The application defines the ideal format. Industrial users demand continuous, snag-free payout. They pull ropes into automated machinery or long-distance rigging setups. Tangled lines cause immediate downtime. For these users, structural support is vital. Spools provide this consistency.
Consumer retail requires a different approach. Shelf space is highly limited. Stores prefer compact packages that hang neatly on pegboards. Consumers typically buy short lengths for temporary utility. In these cases, hanks offer the perfect solution. They display well and unravel easily by hand.
Logistics and storage efficiency heavily influence this decision. Shipping containers have fixed internal volumes. You want to fit as much product as possible into every shipment. Efficient rope packaging maximizes volumetric space. Spools stack predictably and uniformly. Coils save weight by eliminating wooden or plastic cores, but they often leave empty voids between stacks. Hanks pack densely in boxes but require more manual handling. You must balance the core weight against the spatial efficiency.
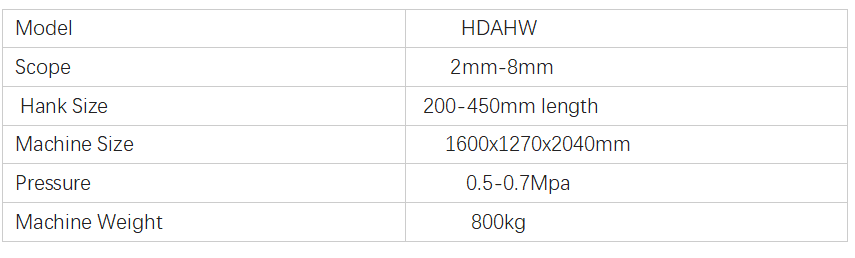
Once you understand your material and user needs, you must evaluate the actual winding formats. Each method requires a specific mechanical approach. They each offer distinct advantages and drawbacks.
Spool winding represents the industry standard for continuous, high-volume production. It involves wrapping the rope around a central cylindrical core. Many spools feature side flanges to contain the material.
This method works best for high-speed automated dispensing. It is ideal for wire ropes, fiber optics, and sensitive synthetic lines. The rigid core prevents the inner layers from crushing. A dedicated spool winding machine delivers exceptional structural integrity. It tightly packs the material in precise, level layers.
However, spools require ongoing inventory management. You must purchase wooden, plastic, or cardboard bobbins constantly. Some modern facilities use coreless spooling. This advanced method winds the rope onto a temporary mandrel. The mandrel collapses and retracts, leaving a self-supporting spool. This saves money on core inventory but limits the package's crush resistance.
Hank winding organizes rope into a folded, looped bundle. It completely eliminates the central core. You secure the bundle with a small wrapper or tie string.
This format is best for retail-length utility ropes. It suits climbing ropes, paracord, and marine dock lines. An industrial hank winder operates with rapid cycle times. It quickly wraps a specific length, cuts it, and discharges the bundle. This optimizes point-of-sale presentation.
Hanks reduce overall packaging weight. They require zero internal cores. Customers love them because they unroll quickly without special stands. However, hanks are generally limited to lengths under 100 meters. Longer lengths become too bulky to support their own weight effectively.
Coil winding creates a large, circular bundle. It resembles a spool but lacks the rigid bobbin. The rope supports itself through careful layer placement.
This method is best for bulk wholesale. It suits large-diameter mooring lines and heavy construction ropes. A heavy-duty coil winder minimizes packaging waste. You only need strapping bands or shrink wrap to secure the final product.
Coiling requires precise traversing. If the machine stacks layers unevenly, the center will collapse. A collapsed coil causes massive tangles during payout. You must maintain strict control over the package build structure.
Winding Method | Best Suited For | Key Advantage | Main Limitation |
|---|---|---|---|
Spool Winding | Industrial use, long lengths, sensitive synthetics | Highest structural integrity and payout speed | Requires ongoing bobbin/core inventory |
Hank Winding | Retail packaging, paracord, short utility lengths | Excellent shelf display, zero core required | Limited to shorter lengths (typically <100m) |
Coil Winding | Heavy marine lines, large diameter construction ropes | Minimal packaging waste, great for bulk transport | Requires precise traversing to prevent center collapse |
Selecting the format is only the first step. You must now evaluate the machinery that executes the process. A poorly designed rope winding machine ruins good material. You must scrutinize several technical criteria before making a capital investment.
First, evaluate the precision of the tension control systems. This is the most critical component. Closed-loop tension systems actively monitor the pulling force. They use load cells or dancer arms to read the line pressure in real-time. The controller adjusts the motor speed instantly. Managing optimal winding tension prevents rope stretching. High tension reduces the rope's physical diameter. It permanently degrades the breaking strength. Low tension creates spongy, loose packages that fall apart during transit. You need exact, programmable control.
Next, assess the traverse accuracy. The traverse mechanism guides the rope back and forth across the package width. Synchronized servo-driven traversing is essential. Mechanical pitch drives often slip or wear unevenly. Servo systems mathematically lock the traverse speed to the spindle rotation. This ensures perfectly flat, even layers. Flat layers prevent the rope from diving into lower layers. Snag-free payout relies entirely on this precision.
You must also consider changeover efficiency. Production lines rarely run one product forever. You will change rope diameters, colors, and spool sizes frequently. How long does this take? Evaluate the tooling design. Quick-release pintles save hours of labor. Recipe-driven software allows operators to change pitch settings instantly via a screen. Slow changeovers kill daily throughput.
Finally, review the integration capabilities. Your winder does not operate in a vacuum. It sits downstream from extruders, braiders, or twisters. It must synchronize seamlessly with upstream equipment. If the braider slows down, the winder must match that speed exactly. Look for modern PLC (Programmable Logic Controller) systems with open communication protocols. They ensure your entire line runs as one unified system.
Ignoring the minimum tension threshold required for extremely fine synthetic yarns.
Assuming mechanical traverse guides offer the same accuracy as servo-driven guides.
Failing to test the machine's emergency stop synchronization with upstream extruders.
Buying the equipment is only half the battle. Installing and running it presents a new set of challenges. You must prepare your facility for these implementation realities.
Footprint and layout limitations often derail projects. Modern winding lines require significant physical space. You need room for the machine itself. You also need space for dancer accumulators. Accumulators store excess rope while the machine changes empty spools. This allows the upstream line to run continuously. You must measure your floor space carefully. Factor in aisle widths for forklift access. Operators need safe zones to maneuver heavy bobbins.
Safety and compliance present strict requirements. Regional industrial safety standards are non-negotiable. You must comply with CE (Europe) or OSHA (USA) regulations. Look for comprehensive machinery guarding. Moving spindles and traverse guides pose severe pinch hazards. Demand interlocked safety doors. If an operator opens a door, the machine must stop instantly. Emergency stop circuits must integrate with the entire production line.
Operator training overhead is a hidden challenge. Complex HMI (Human-Machine Interface) panels confuse new staff. If the software is poorly designed, operators will make mistakes. They will input wrong traverse pitches or tension setpoints. This ruins entire production runs. You need intuitive, visual software. The system should store specific product recipes. Operators should simply select "10mm Nylon Spool" and let the machine load the parameters automatically.
Maintenance downtime directly impacts your profitability. Every mechanical system experiences wear and tear. Traverse guides handle miles of abrasive rope daily. Tensioner pulleys accumulate dirt and fibers. You must assess the OEM (Original Equipment Manufacturer). Do they keep spare parts in stock? Can they ship a replacement servo motor overnight? A robust preventative maintenance schedule keeps the line moving. You must train your team to clean sensors and lubricate guides regularly.
Map the entire production floor in 3D CAD before finalizing the equipment order.
Establish dedicated lockout/tagout (LOTO) procedures specific to the new winder.
Require the equipment vendor to provide video-based maintenance tutorials.
Stock critical wear items (ceramic guides, drive belts) on your own shelves on day one.
You know what you need. Now you must select the right vendor to build it. A structured evaluation process protects your investment. Do not buy based on glossy brochures alone.
Begin by defining your success metrics clearly. Establish rigid baseline requirements. What is your required throughput in meters per minute? What is the absolute maximum and minimum diameter range the machine must handle? Define your target coil weight or spool dimensions. Document these metrics in a formal specification sheet. Make vendors guarantee they can meet these exact numbers.
Next, insist on requesting sample runs. This is your Proof of Concept (POC). Never buy a machine without testing it first. Every rope material behaves differently under tension. Send sample spools of your hardest-to-wind materials to the vendor. Have them wind it on their demo equipment. Demand a video of the process. Better yet, visit their facility to inspect the final package. Check the tension stability yourself. If the layers are loose or the rope is stretched, walk away.
Finally, rely on rigorous Factory Acceptance Testing (FAT). The FAT is your final safeguard. Include non-negotiable clauses in your purchasing contract. The vendor must prove the machine meets every spec before it leaves their floor. You must witness the FAT, either in person or via live video. Test the machine at its maximum rated speed. Trigger safety sensors to ensure proper shutdown. Run the smallest and largest diameters to verify changeover times. If the machine fails a test, the vendor must fix it before shipping. Once it arrives at your facility, it is too late to demand major structural changes.
Selecting the ideal rope packaging format dictates your product's market success. Matching the winding method—whether spool, hank, or coil—to the material characteristics and end-user demands is step one. Acquiring specialized equipment that executes that method without degrading the product is step two.
You must prioritize precision tension control and servo-driven traversing. These technologies protect your rope's material memory and ensure snag-free dispensing. Carefully evaluate your facility's footprint and operator capabilities before finalizing any layout.
Your next action is to audit your current packaging bottlenecks. Calculate the scrap rate caused by poor tensioning on your existing lines. Document your space constraints. Finally, consult with specialized equipment manufacturers to map out a fully automated, synchronized solution tailored to your exact fibers.
A: Generally, no. While some modular systems exist, industrial-scale efficiency requires purpose-built machines (or distinct winding heads) for each format due to vastly different mechanical actions.
A: Excessive tension alters the rope's diameter and breaking strength; insufficient tension results in collapsing coils or spools that tangle during payout.
A: Depending on labor offsets and throughput increases, standard industrial winders typically achieve ROI within 18 to 36 months, factoring in reduced material scrap.